
KF 3114 / 28
Plate processing centre for complete steel processing from one single source

KF 3114 / 28 BENEFITS AT A GLANCE
- Diverse manufacturing technologies
- Milling as standard function of the machine
- Powerful drives
- Higher spindle speed
- Optional downholder roll for optimum plate contact pressure
- Increased stability
- 14/28-place tool changer
- Less space needed for measuring carriage
- Measuring carriage to optimise plate fixation
- Increased traversing speed of axes
FEATURES
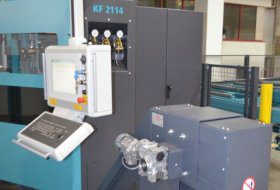
Convenient operation of the system
Plain-text display of machine data and possible error messages
Good observation of the processes and rapid intervention in case of disturbance
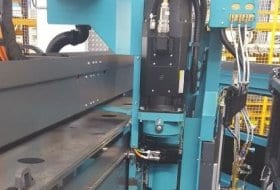
Low wear and low maintenance
Drill carriage mounted on dual play-free, pre-stressed linear guides
Robust mountig for high precision when drilling
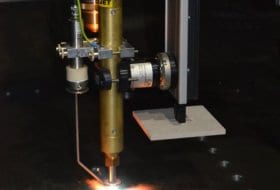
Universal, economical gas cutting process
Universally implementable gas cutting unit built onto the drilling unit
Automatic height adjustment of the cutting unit
Fully automatic processing possible
Automatic disposal of small parts in a removable finished-parts container
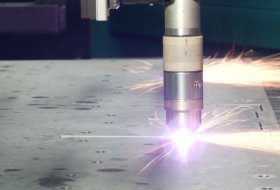
High cutting speed
Highest cutting performance and optimum cutting quality
In addition a high-performance plasma cutting machine can optionally be used
Common cut and cross-cut technology generates significantly less waste
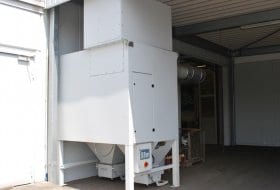
Dust free work environment
System with pre-separator and dust collection container
Filtering unit with eight cartridges in flame retardant design
Automatic filter cleaning
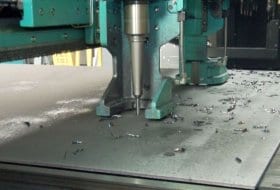
Double throughput
Can be expanded with an additional drilling/gas-cutting unit (autogenous and/or plasma)
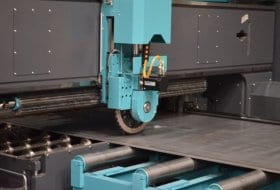
Fast marking process
Fast, high-quality marking process for applying letters and numbers
Marking depth to 1 mm regardless of material and plate thickness
Imprint still clearly visible after galvanizing or painting

Material marking by means of a milling tool
Application of numbers + letters and reference boundaries for welding add-on pieces
DSTV-Data import
Use of high-speed carbide tools
Machine operation with most up-to-date software
Easy data import and export
Automatic or manual nesting
Partial programming possibility via NC-DSTV, DXF or DWG files
Integrated drawing program or macros
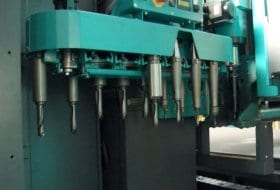
Short changing times for tools
Automatic tool change on the drilling unit for the most common tool sizes
Tool change unit consists of a chain change system directly attached to the portal
Tool change automatically sets the correct speed and feed-rate values
Automatic drill length sensing
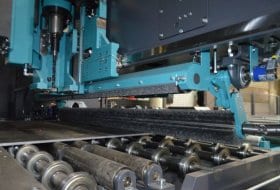
Swarf brush
Fully automated swarf removal before thermal cutting
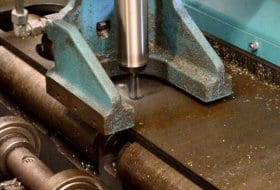
Downholder and downholder roll
Minimises vibrations and thus increasing machining quality and prolonging tool life
Hold-down device is used with extensive milling operations
TECHNICAL DATA
| Dimensions (L x W x H) | 15500 x 8000 x 5000 | |
| Weight | kg | approx. 11000 |
| Supply and discharge side | Drilling | |
| Thermal cutting | ||
| Contour Marking | ||
| Milling | ||
| Threading | ||
| Reducing | ||
| Signing | ||
| Feedrate | mm/min | 2000 |
| working range Plate | mm | 3100x6.000 |
| Drilling unit horizontal (Z- and W-axis) | Pieces | 1 / 2 |
| Drill Size | mm | 6,8 - 50 |
| Number of tools per axis | Pieces | 14 |
| Drive power axe | kW | 34,5 kW |
| Spindle speed max. | min-1 | 3500 |
| Sheet starting material sheet width | mm | 220 - 2100 |
| Sheet starting material sheet length | mm | 500 - 6000 (12000) |
| Sheet starting material sheet thickness | mm | 6 - 100 |
| Toolchanger x Magazine places | Pieces | 1 x 14 (2 x 14) |
| Tools | Carbide Tools | |
| HSS-Tools | ||
| Solid Carbide Tools | ||
| Degree of Automation | automatic sorting of trim and remnant cuts | |
| Full-Automatic | ||
| Material class | Steel | |
| Working processes | Plate | |
| Component length max. | mm | 60 x 60 / 2100 x 6000 (12000) |